How to improve chemical plant piping reliability: material, seamless tube and NDT
Most chemical plant piping failures trace back to creep fatigue, chloride stress corrosion or weld defects. A practical look at material selection, seamless forming and micro-scale NDT.
By Dakai Steel Technical Team
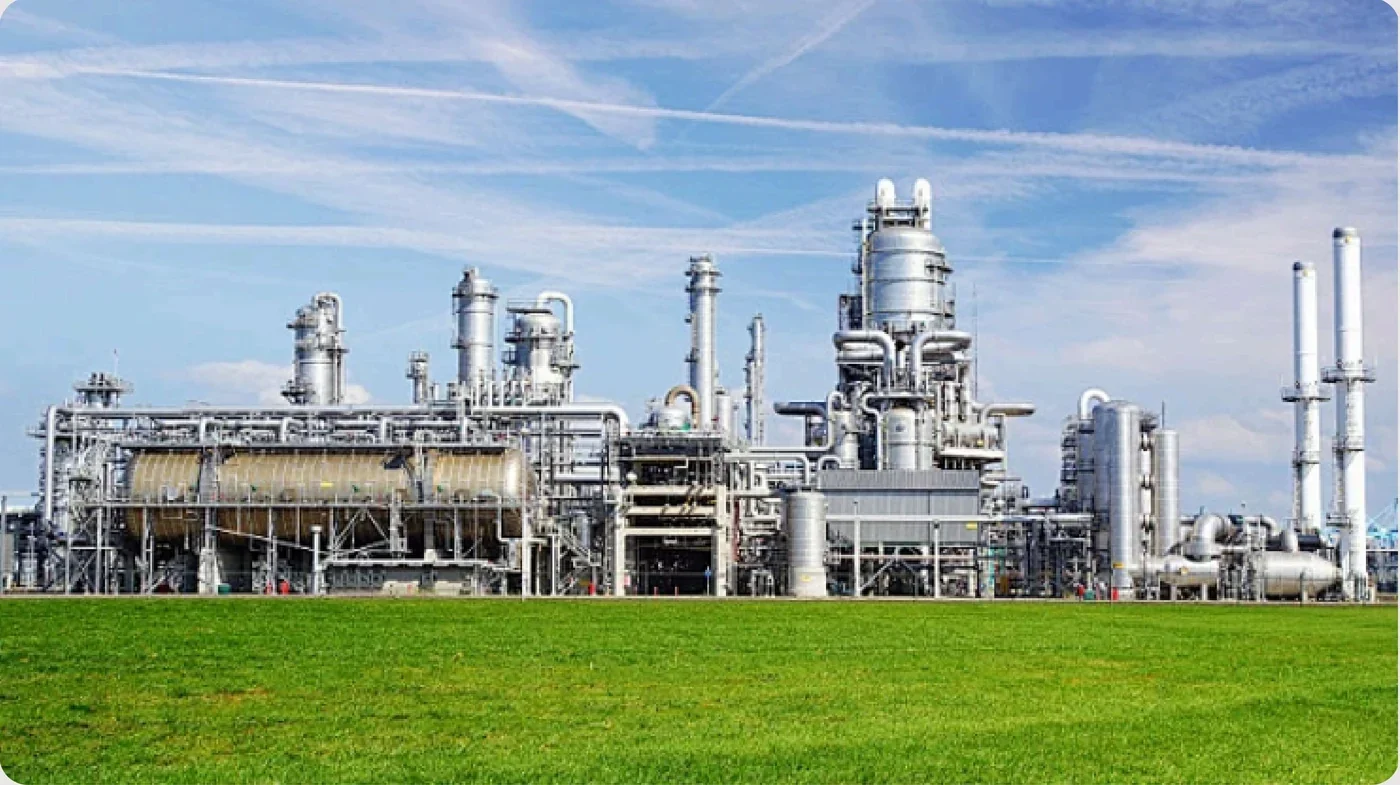
In coal chemical, fine chemical and petrochemical plants, fluid piping carries the whole energy cycle and material transfer. Large units move thousands of tonnes of hot heat-transfer oil, high-pressure hydrogen and corrosive acids every day.
Turning feedstock into product takes dozens to hundreds of catalytic, cracking and synthesis steps, all linked by reactors, exchangers, pumps and valves. One leak or rupture can trip the entire unit.
Failures cluster in three places: creep fatigue under combined high temperature and pressure; stress corrosion cracking driven by residual chlorides; and hidden defects left by wrong material selection or undetected weld flaws.
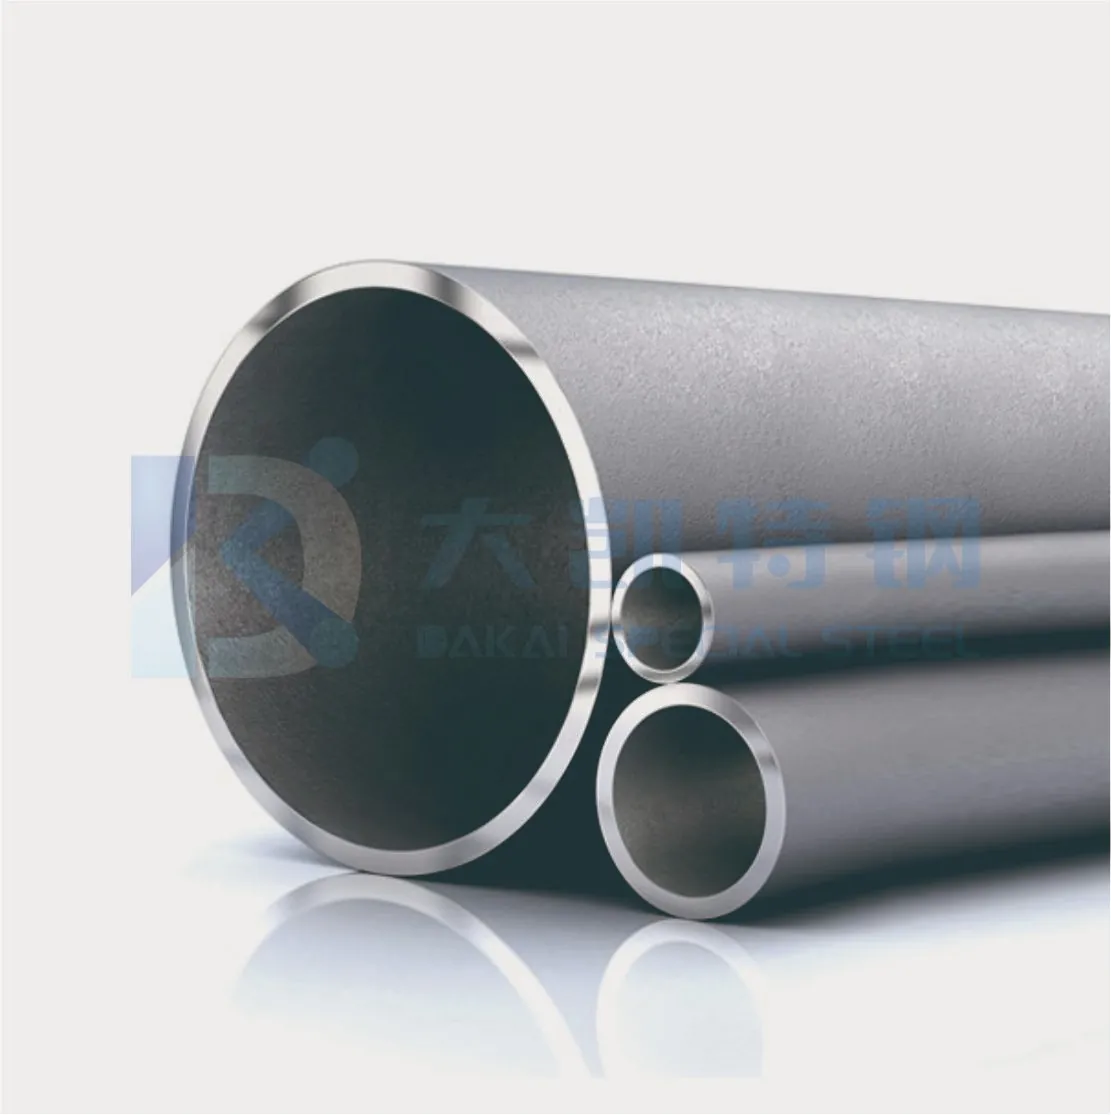
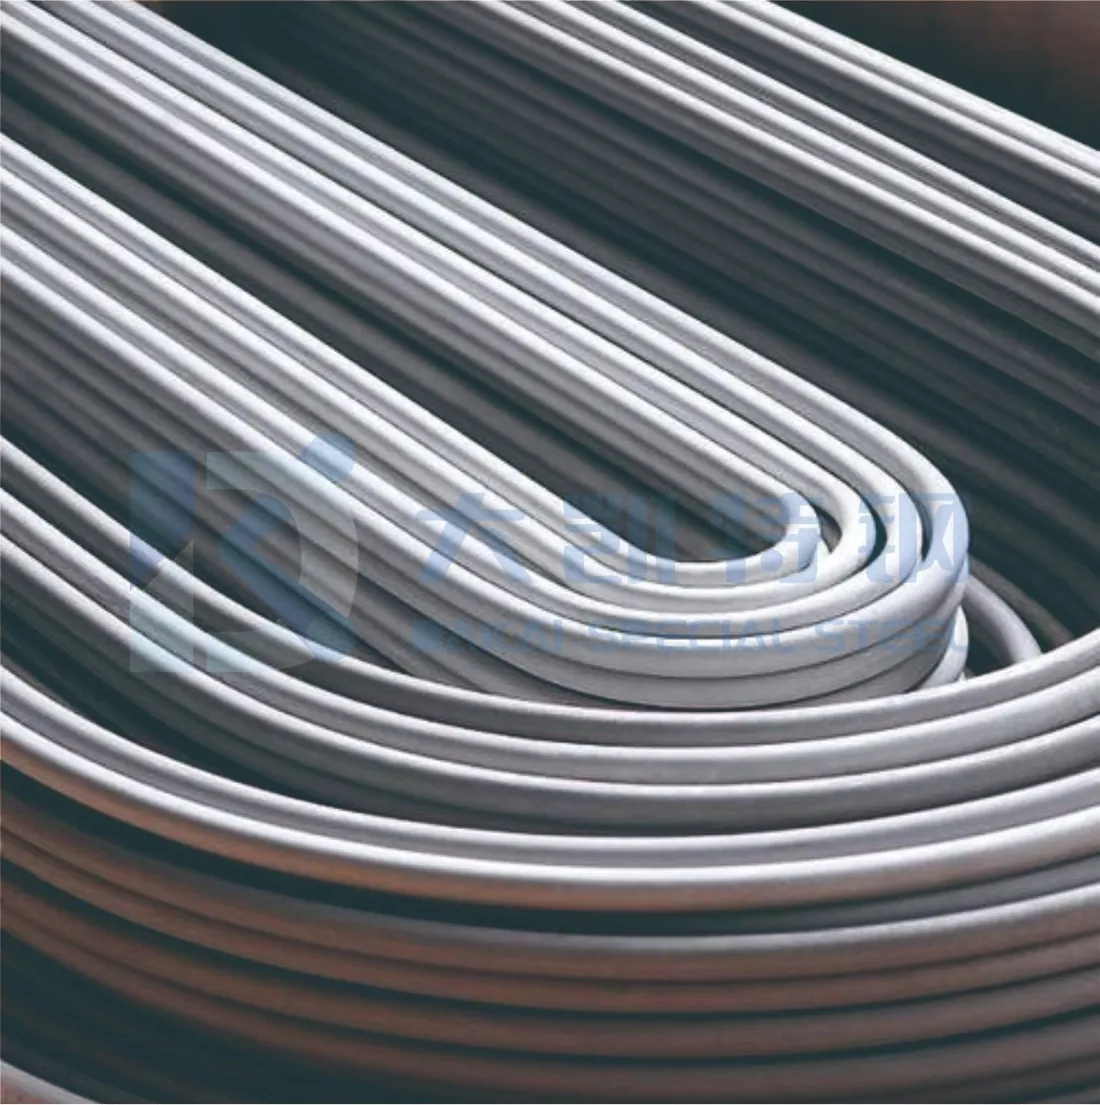
Leading operators work upstream on material and quality control: special alloys matched to the medium; cold-drawn or cold-rolled seamless tube instead of welded pipe in extreme duty; and micro-scale NDT stricter than national standards.
For high-chloride and strong acid or caustic service, 2205 and 2507 duplex grades balance chromium, nickel, molybdenum and nitrogen into an austenite-ferrite structure, supplied at OD 6–630 mm and WT 1–50 mm, plus non-standard sizes.
Testing is coordinated by a digital control centre: energy optimisation, product inspection and trials, and traceable digital records work together, so each tube is documented from billet piercing to shipment.